Hot-dip galvanizing is one of the most effective methods of protecting steel against corrosion. In our plant, we treat it as a stage just as important as the production of the components themselves. The zinc coating is meant to last for decades, which is why we take care of every detail of our work. We protect structures in demanding atmospheric, industrial and mechanical conditions, and we carry out every stage of the process deliberately and with full responsibility.
Zinc is a metallic element present in air, soil and water. It is harmless to the environment and can be recycled. These properties mean that a layer of zinc effectively protects steel against corrosion and is safe for its surroundings. Below we describe how we work and what makes the coatings we create durable, stable and a source of long-term safety and high operating efficiency.
Surface preparation in the hot-dip galvanizing process
Steel arriving at our plant is not yet ready for a permanent bond with zinc. It carries residues from production processes, layers of grease and lubricants, mill scale, traces of corrosion and contamination from transport and storage. Because none of these cooperates with zinc, the surface of the structure must be cleaned precisely and evenly.
The first stage we carry out is degreasing. The steel goes into chemical baths, where we remove residues of oils, greases and any organic substances accumulated during production, transport or storage. This process reveals the actual condition of the surface, prepares it for the following operations and eliminates anything that could disrupt the chemical reactions in later stages. Degreased steel is still not suitable for galvanizing, but it is now clean enough to move on to the next phase of treatment.
Next we carry out pickling in an acid solution. This is a stage of great importance, because we remove mill scale, oxidation products and the hard, hard-to-break layers formed during earlier metalworking processes. The material uncovered in this way gains a structure that allows a durable and uniform bond with molten zinc. It is at this moment that we can assess the actual quality of the surface, notice minor irregularities or cutting residues and, where necessary, correct them before moving on to the next stages.
After pickling is finished, we move on to rinsing and fluxing. We remove acid residues and then apply flux, which forms a thin, even layer that protects the steel against immediate oxidation. We prepare the surface so that zinc can react with it fully, and we ensure the highest quality of the coating. This is a stage invisible to the naked eye, but its importance is enormous, because it is the flux that determines whether zinc bonds with steel evenly and permanently. Without this preparation, the coating would be unstable, with non-uniform areas and weakened adhesion.
Only after the surface has been properly prepared can we move on to the actual galvanizing process.
Hot-dip galvanizing at Strumet – the reaction of zinc with steel
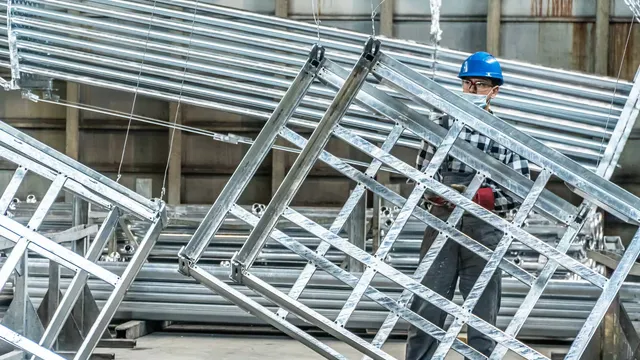
Once the elements are prepared, they go into a galvanizing bath at a temperature of approximately 450 °C. Under these conditions, zinc becomes liquid and comes into direct contact with the steel surface. At this moment diffusion begins, that is, zinc penetrates the structure of the metal and forms alloy layers. The coating we create this way is not simply applied to the surface. It forms as a result of the reaction between zinc and steel, which gives it exceptional stability and resistance to loads that could damage other coatings. Each element gains a layered structure that is resistant to damage and to weather conditions.
During immersion, each element reacts slightly differently. We take its specifics into account and adjust the immersion time so that the coating is uniform and reaches the appropriate thickness. We maintain stable bath parameters and monitor the entire process, because even the smallest deviations can affect the final result. When we lift an element out of the bath, the zinc begins to solidify and sets its structure. The cooling process is essential – it cannot be accelerated or skipped. Proper cooling gives the coating its full mechanical properties, which allow the structure to work in harsh conditions for many years.
Quality control in Strumet's hot-dip galvanizing process
After galvanizing is complete, every element undergoes quality control. We do not limit ourselves to checking compliance with the PN-EN ISO 1461 standard, because standards define minimum values, and our goal is to obtain a stable coating with parameters that ensure long-term resistance. We analyze the thickness of the layer, its uniformity and its continuity. We also check edges and places particularly exposed to process disturbances, such as welds or recesses. If any irregularities appear, the element goes back for further treatment or is put through the process again.
We treat quality control as one of the most important stages of the entire process. We check carefully whether every earlier step was performed correctly and whether the coating has reached the intended performance parameters. Only in this way can we be sure that every element leaving our plant will be durable and resistant to external factors.
A durable zinc coating, resistant for decades
The coatings we create in the hot-dip galvanizing process wear down extremely slowly. In a temperate climate, the annual loss is usually only 1-2 micrometers. With a coating thickness of 70-100 micrometers this means protection for up to 100 years. Depending on conditions, the structure remains fully protected even for several decades, without any need for intervention on our part.
We consider the exceptional durability of the coating one of the greatest advantages of hot-dip galvanizing. It requires no additional maintenance or renewal of the coating. The structure can work in full sun, under snow, in a humid or dry environment, with dynamic temperature changes, and the coating retains its properties and reliability. Such a level of resistance translates directly into economic benefits, because galvanizing done once eliminates the need for servicing or renovation, which significantly reduces operating costs over the entire service life of the structure.
Why our process is stable and effective
At Strumet, we focus on precision and repeatability at every stage of hot-dip galvanizing. We prepare the surface, pickle, flux, immerse in zinc and carefully control quality. Every step is important, and an omission or inaccuracy could affect the durability of the coating, for which we always guarantee full parameters.
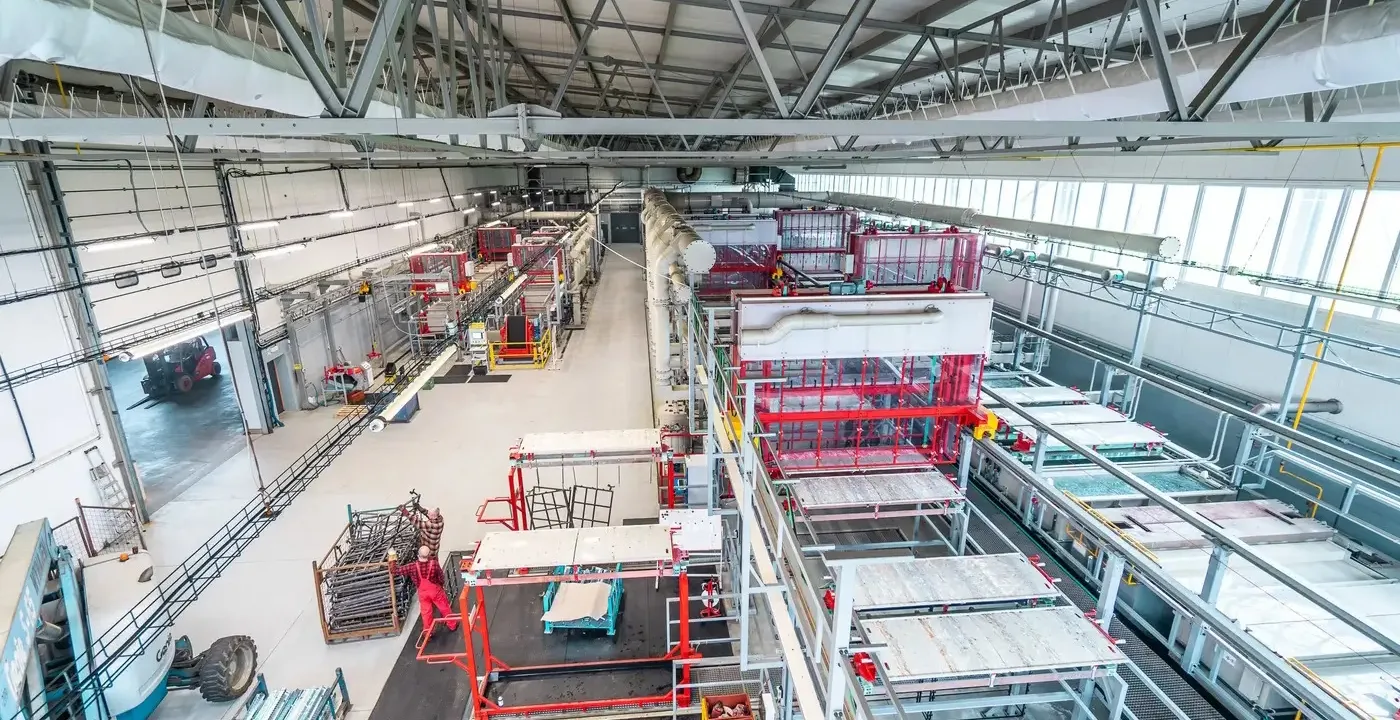
Our process line allows us to carry out hot-dip galvanizing under fully controlled conditions. We watch over every stage – the baths, the temperature and the composition of the solutions – and we observe the reactions of the steel in real time. This allows us to create exceptionally resistant and durable coatings, regardless of the shape or size of the element. The result is reliable and long-lasting, and steel protected with hot-dip zinc retains its properties for decades. The hot-dip galvanizing process is not a metallurgical process, so it is not harmful to the environment. Every customer can be sure that their structures will remain stable, reliable and ready to work in the toughest conditions, with no need for additional maintenance.