
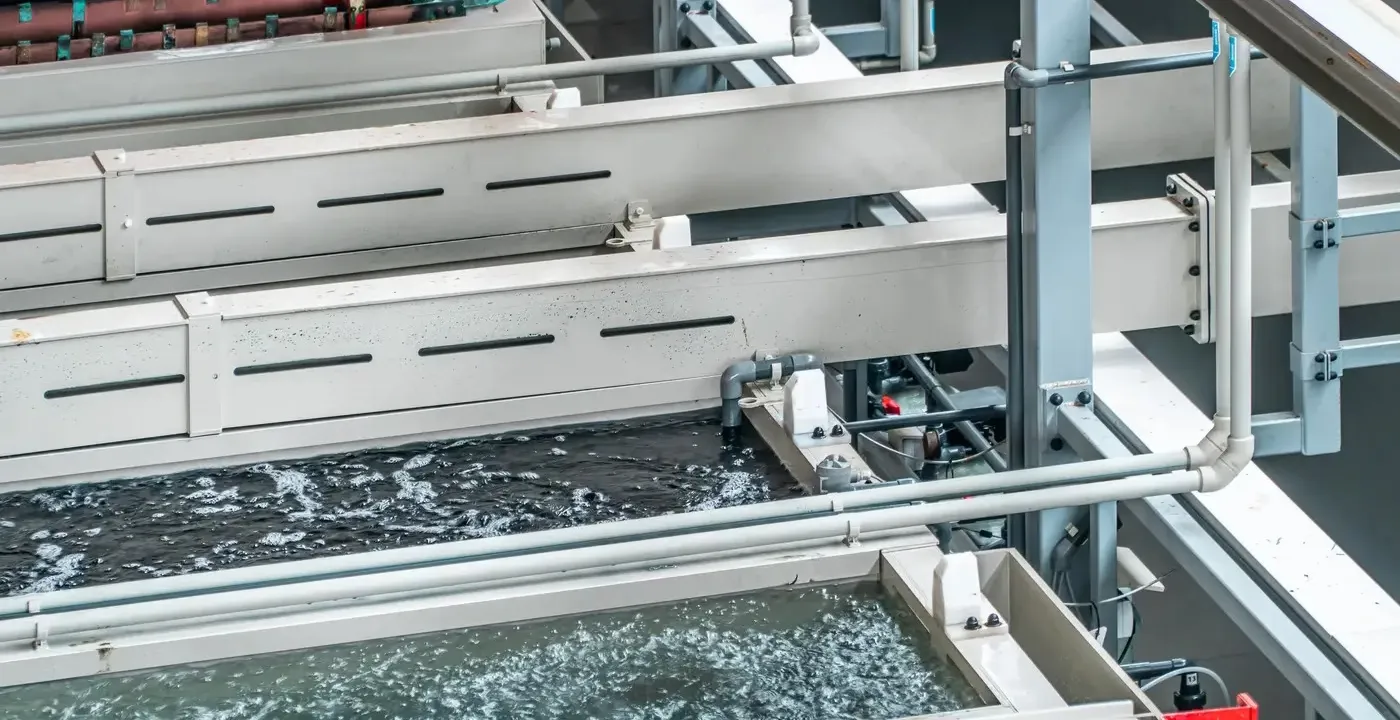
Metal electroplating is a technology in which the end result shows very precisely how the process was run. It cannot be corrected at the last stage, nor can minor errors be masked visually. If the surface was prepared carelessly, the bath was run unstably, or the electrical parameters were set too aggressively or too conservatively, the coating will sooner or later reveal it. Sometimes this is visible right after the part is taken out of the bath, and sometimes only after several months of work in real conditions. That is exactly why electroplating has long been regarded as a demanding process, but at the same time one of the most predictable when it is run consciously.
In practice, electroplating is rarely limited to corrosion protection alone. It makes it possible to influence the way the metal surface reacts to moisture, oxygen, friction, electric current or contact with chemical substances. Very often it is a thin layer a few or a dozen or so micrometers thick that determines the durability of a part, not the base material itself, even if the latter theoretically has very good strength parameters.
What actually happens in the electroplating bath
The entire process is based on electrochemical phenomena. The part to be coated works as the cathode, while the bath contains ions of the coating metal. When voltage is applied, the ions begin to move in the electric field and are reduced on the surface of the part. This moment is often perceived as a simple stage of metal deposition, but in reality it is a complex structural process.
First, nucleation sites appear on the surface, that is, points where the crystalline structure begins to build up. Their distribution depends both on the cleanliness of the surface and on the local distribution of the electric field. Only later do the crystallites begin to grow and merge into a continuous layer. How this stage proceeds has a direct impact on the smoothness of the coating, its adhesion and its resistance over long service. In practice this means that two parts run in the same bath with identical parameters can behave completely differently if they differ even slightly in the degree of surface preparation.
Current density as a regulator of coating growth
The way the deposit grows is influenced most strongly by current density. Typical ranges lie between 0.5 and 10 A/dm², but what is key is not the value itself but its relationship to the geometry of the part and the character of the bath. It is current density that determines the rate of ion reduction and whether the growth of crystallites will be orderly or too aggressive.
At high current density, the deposit builds up quickly, but mainly in the places the current reaches most easily. Edges and corners start to collect excess metal, and internal stresses appear in the structure of the coating. Over time, they can lead to microcracks or reduced corrosion resistance. Conversely, too low a current density causes slow deposit growth, which can be porous and less mechanically resistant. In practice, the best results come from working in a stable, moderate range, even if that means a longer process time.
Current shadowing and the role of part geometry
At this point the topic of current shadowing naturally arises. Electric current always reaches protruding surfaces more intensely than recesses, holes or the insides of profiles. This phenomenon results directly from the distribution of the electric field in the bath and accompanies every electroplating process.
In practice, this means that the geometry of the part has an enormous impact on the uniformity of the coating. Edges tend to build up a thicker layer, while recesses require a longer process time or a change in the way the part is racked. Very often, simply correcting the orientation of the part in the bath yields a much more even coating than changing the bath composition or the voltage.
The electroplating bath as a system that is constantly changing
The uniformity and repeatability of the process are also affected by the fact that an electroplating bath is not a static system. During operation, the concentration of metal ions changes, process additives are consumed, and pH, conductivity and temperature fluctuate. Typical operating conditions fall within the range of 18-35°C, with a pH of around 4-5 for acid baths and 12-14 for alkaline baths.
Brighteners and leveling agents affect the way zinc crystallites grow, and thus the appearance and uniformity of the coating. Their consumption is not constant and depends largely on the geometry of the parts being processed. In practice, this means that even small changes in the bath composition can quickly alter the character of the deposit and the quality of the coating.
Surface preparation – the stage that determines quality
At this point everything naturally comes down to surface preparation. Electroplating very quickly reveals mistakes made at this stage. Residues of oils, silicones, scale or machining by-products lead to local loss of adhesion, blisters or discontinuities in the coating. Some of these defects are not visible directly after the process, but show up in the first period of service.
That is why every electroplating process begins with:
- degreasing,
- pickling,
- rinsing,
- activation.
Types of electroplated coatings and their functions
Standard electroplated coating thicknesses fall in the range of 5-30 µm, which makes it possible to maintain very good dimensional accuracy even in precision parts. Depending on operating requirements, various coating metals are used:
- zinc provides corrosion protection
- nickel increases chemical and mechanical resistance
- copper improves conductivity
- tin protects electrical contacts
- chromium increases abrasion resistance
Metal electroplating at Strumet
At Strumet, metal electroplating is treated as a fully thought-out technological process, not a quick step at the end of production. Before a part goes into the bath, we analyze the material, the geometry and the conditions in which it will later work. We operate rack and barrel lines, which lets us match the technology both to large components and to small, precision parts. At every stage we monitor the bath composition, pH, temperature and current density. It is these parameters that determine the structure of the coating and its behavior in service, which is why we run the process in a stable and repeatable manner.





