
Steel corrosion costs industrialized countries several percent of GDP every year. Fortunately, it can be effectively counteracted – with real savings. One of the most effective and cost-efficient methods of protecting steel components against rust is zinc electroplating. That is why, in the machinery, automotive and energy industries, in construction and in telecommunications, a proven electroplating shop is an invaluable business partner. Let us take a closer look at what hides behind this name and what standards a modern galvanizing plant should meet.
What is an electroplating shop and what is it for?
In short, an electroplating shop is a specialized industrial plant that deals with the electrolytic application of metallic coatings to steel components. The Strumet electroplating shop specializes in zinc electroplating – a process in which a thin layer of zinc is deposited on the metal surface with the help of direct current and electrolytic baths.
The zinc coating performs two functions here. First and most importantly, it forms a corrosion barrier. Zinc protects steel both mechanically, by isolating it from the environment, and electrochemically – as a metal with a lower electrochemical potential than iron, it oxidizes instead of the protected substrate. Thanks to these properties, metal electroplating is one of the basic means of protecting metal in conditions of exposure to moisture, aggressive chemical media or changing weather conditions. The second aspect is aesthetics. Zinc coatings, available in various finishing variants, give the structure a uniform appearance.
The zinc electroplating process step by step
Zinc electroplating is a multi-stage technological process whose quality depends equally on the electrolysis parameters and on the care with which the surface was prepared beforehand. Every stage has a direct impact on the adhesion of the coating, its uniformity and its protective properties.
Surface preparation: degreasing and pickling
In the preparation stage, steel components pass through several successive tanks. Degreasing removes organic contaminants from the metal: oils, greases, anti-spatter agents used in welding and other surface-active substances that would prevent even zinc deposition. The next step is acid pickling, which removes iron oxides, mill scale and rust, exposing a clean, metallically active substrate. The pickling time depends on the condition of the load surface; before the electroplating bath, all components are also rinsed multiple times.
Electrolysis and application of the zinc coating
The actual electroplating stage involves immersing the prepared components in an electrolytic bath containing zinc salts and passing direct current through the system. The mechanism is simple: zinc ions (Zn²⁺) migrate under the influence of the electric field toward the cathode (that is, the part being galvanized) and are reduced to metallic zinc, which deposits on the surface. The rate at which the coating builds up, its texture and its mechanical properties depend on:
- current density (A/dm²),
- bath temperature and composition,
- pH value,
- presence and concentration of organic additives (brighteners, levelers, etc.).
These parameters are not constant, so to guarantee process repeatability, they must be continuously monitored by computer systems and corrected by technologists.
Passivation and types of finishes
Freshly galvanized components – although already protected by zinc – require additional chemical treatment called passivation. It involves immersing the structure in chromate or chromium-free solutions, which form a thin, compact layer of oxides and hydroxides on the zinc surface. Depending on the composition of the passivation bath and the contact time, the following finishing variants are possible:
- blue (clear) passivation – the thinnest passivation layer with a slight rainbow sheen;
- yellow (gold) passivation – a thicker chromate layer, a distinct golden-yellow color, increased corrosion resistance;
- black passivation – a layer with silver or nickel salts added to the bath, an aesthetic effect similar to blackening.
At Strumet we use chromium-free passivation, based among other things on titanium compounds. This treatment significantly extends the coating's resistance to white corrosion (zinc corrosion) and improves its barrier properties, and of the available methods it is also the most environmentally friendly.
Rack and barrel lines at Strumet – a modern electroplating shop in Silesia
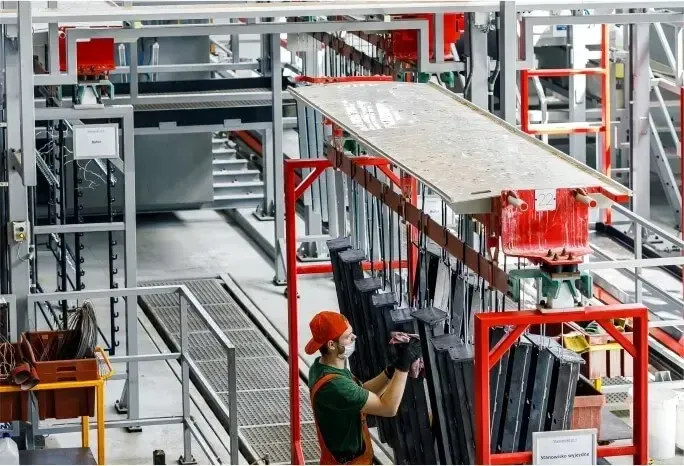
Strumet can boast more than 30 years of experience in the industry, and the electroplating shop in Silesia we launched in mid-2020 is among the most modern zinc electroplating installations in Poland. At the heart of the plant are two fully automated production lines. The rack line is designed to handle larger structural components. It accepts parts up to 2.8 m long × 0.8 m wide × 1.8 m deep, with a maximum load weight of 600 kg per traverse and a surface area of up to 1,200 dm² per traverse. The barrel line is used for galvanizing small parts (connectors, bolts, nuts, washers, clamps) in bulk.
Both lines are equipped with autonomous transporters that move components between successive process tanks without operator involvement. Bath parameters – temperature, pH, conductivity, zinc salt concentration and organic additives – are recorded and supervised by a computer monitoring system in real time. The correct composition of the process solutions is overseen by chemists with their own analytical laboratory.
Why outsource zinc electroplating? Quality, lead times and ecology
Different types of electroplating are used in different industries; the specific solution is always matched to the scale and the expected effect. When it comes to zinc electroplating, one of its greatest advantages is the ability to precisely control the thickness of the applied coating. Depending on the customer's requirements and the operating conditions of the structure, the plant offers coatings in the range of 3–25 µm (with full repeatability of results!). In addition, Strumet's modern infrastructure and processing capacity translate into competitive lead times – up to 24 hours for orders weighing up to 100 kg and a maximum of 72 hours for a weight of 1–3 t. The daily throughput of our electroplating shop reaches 20,000 kg, which makes it one of the largest and most efficient in the country.
Finally, it is worth mentioning that Strumet's operations are always guided by care for nature. Thanks to an advanced system for treating and regenerating process solutions, the process baths operate in a closed loop (the installation does not generate industrial wastewater). This solution complies with BAT standards and meets the strict environmental requirements imposed on modern electroplating plants in the European Union.
FAQ – the most common questions about electroplating shops
How does zinc electroplating differ from hot-dip galvanizing?
Hot-dip galvanizing (HDG) involves immersing steel components in liquid zinc at approx. 450°C. The resulting coating is very durable, but thicker and more locally variable, especially in corners and hard-to-reach places. Zinc electroplating (electrolytic) takes place at ambient temperature, using direct current. It produces much thinner and more uniform coatings (3–25 µm), which is why it is the recommended solution for threaded components, precision machine parts and other components requiring tight dimensional tolerances.
What zinc coating thickness can be achieved with the electrolytic method?
In the standard zinc electroplating process, coatings in the range of 3–25 µm are obtained. The thicknesses most commonly used in industry are 5–12 µm for components used indoors and 12–25 µm for components exposed to weather or aggressive media. Coating thickness is a controlled parameter and is confirmed by measurements after the process is completed.
What are the minimum and maximum dimensions of parts for zinc electroplating?
The rack line at Strumet handles components with dimensions not exceeding 2.8 m × 0.8 m × 1.8 m (length × width × depth), with a load weight of up to 600 kg per traverse. When two dimensions are close to the limits, prior technical consultation is required. The barrel line is intended for small bulk components – the required minimum load is 20 kg per barrel, with no defined maximum size limit for a single part (apart from the obvious limitations of the barrel volume).
How long does it take to complete an order at the Strumet electroplating shop?
Orders of up to 100 kg are completed within 24 hours, from 100 kg to 1 t – within 48 hours, from 1 to 3 t – within 72 hours. For orders above 3 t, the lead time is set individually. This is one of the shortest turnaround times available on the Polish zinc electroplating services market.





