
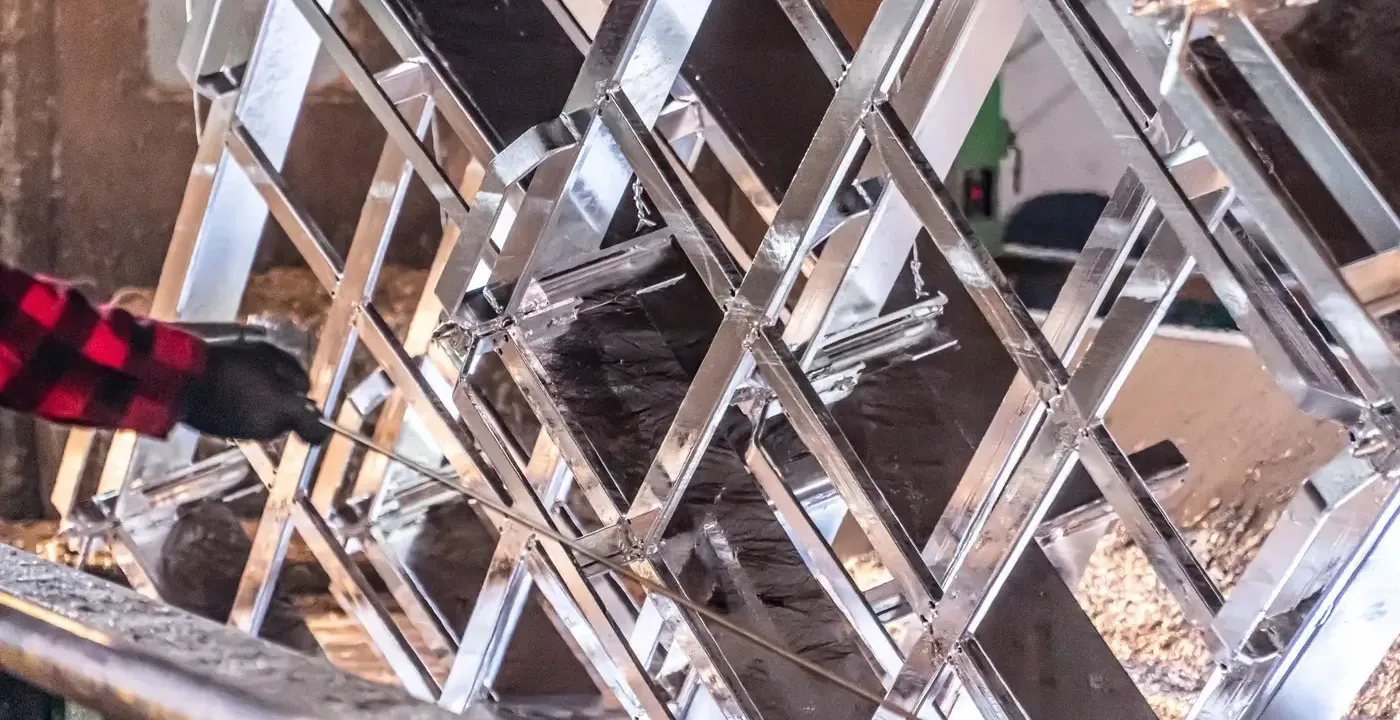
Electrolytic zinc plating is a thin layer of zinc applied to steel in an electrolytic bath, which protects the metal against corrosion but does not change its shape or dimensions.
The coating forms evenly and accurately follows the surface of the component, so it works well for parts that must fit together and look good even after protection.
We run the process under electrochemical conditions, without heating the steel to high temperatures. The steel component acts as the cathode, and zinc is deposited on its surface from the electrolyte solution. The absence of thermal loads eliminates the risk of distortion and structural changes in the material, which is particularly important for thin-walled, threaded and precision components. This is one of the main differences compared with hot-dip galvanizing and at the same time one of the greatest advantages of this technology.
How Electrochemical Deposition of Zinc on Steel Works
During electrolytic zinc plating, Zn²⁺ zinc ions move in the electric field toward the surface of the part and are reduced. Zinc is deposited in the form of crystallites that gradually build up a compact protective layer. Unlike in hot-dip galvanizing, no Fe-Zn diffusion reactions take place here, so the coating does not become part of the steel structure but remains a deposited layer of precisely controlled thickness.
The typical thickness of a zinc coating obtained by the electrolytic method is in the range of 5-15 µm, although it can be modified depending on technical requirements. Such a range makes it possible to maintain the dimensional tolerances of threads, fits and mating surfaces, which is crucial in many applications.
Current Density and Its Effect on Zinc Coating Quality
Throughout the process, current density is of key importance. It determines the rate at which the coating grows and what its structure looks like. With properly selected values, most often in the range of 1 to 5 A/dm², zinc deposits evenly and forms a compact, fine-grained layer without excessive stresses. Too high a current density causes excessive zinc build-up on edges and corners. Higher internal stresses appear, and the coating becomes more susceptible to white corrosion. In turn, too low a current density leads to a porous deposit, less well bonded to the substrate and less resistant in service. In practice, it is current control that determines a calm and repeatable zinc plating run.
Coating uniformity is also affected by current shadowing. This phenomenon results from the geometry of the part and the distribution of the electric field in the bath. Current always reaches edges more easily than recesses, so the way the component is racked or its movement in the barrel has a direct impact on the final result. Well-planned positioning of the part helps limit this phenomenon and obtain an even layer of zinc across the entire surface.
Zinc Baths and Their Importance in the Process
In practice, most work is done in alkaline baths and acid baths, and the choice between them depends on the type of part and the desired effect. Alkaline baths handle current distribution well and allow components with complex geometry to be coated evenly. They operate in a high pH range, usually 12-14, at a moderate temperature of 20-30°C. This is a stable and predictable solution, especially for more difficult shapes.
Acid baths are chosen where the appearance of the surface matters. They make it possible to obtain very smooth, fine-grained coatings, valued especially on visible and precision components. They operate at a lower pH, most often in the range of 4.5-5.5, at temperatures similar to alkaline baths. However, they require tighter control, because they are more sensitive to local current overloads and react faster to parameter deviations. The bath composition is completed by brighteners and levelers, which are responsible for the crystal structure, gloss and surface leveling. Even small changes in their concentration can clearly alter the character of the coating. For this reason baths must be regularly analyzed and adjusted, because it is the chemistry in the background that largely determines the final result of zinc plating.
Preparing the Steel Surface Before Electrolytic Zinc Plating
In electrolytic zinc plating, errors from the earlier stage cannot be hidden. Any residue of grease, silicone or scale, or any mark from machining, very quickly shows up on the surface as local gaps in the coating or uneven zinc deposition. This is the moment when the process clearly shows whether the steel was prepared as it should have been.
That is why the whole cycle always begins with thorough surface preparation. Degreasing, pickling, rinsing and activation are not an add-on but the foundation of the work that follows. We match each of these steps to the type of steel and its actual condition, because a part after machining requires a different approach than a component after cutting or bending. It is this stage that has the greatest influence on coating uniformity and its behavior over time. Especially in the initial period of service, when zinc starts working in real conditions, a well-prepared surface determines whether the coating remains stable or begins to reveal its weak spots.
Passivation of the Zinc Coating and Its Corrosion Resistance
After zinc plating we carry out passivation, whose task is to stabilize the freshly deposited zinc and limit its reactivity. Modern processes use chromium-free passivation based on titanium and zirconium compounds, which improves resistance to white corrosion and meets current environmental requirements.
In moderate environments, the rate at which a zinc coating is consumed averages 1-2 µm per year, which with a suitably selected thickness provides many years of protection for steel components. In more aggressive environments, the quality of passivation and the stability of the entire zinc plating process are of key importance.
Applications of Electrolytically Deposited Zinc Coatings
- threaded components, where maintaining exact dimensions and correct fit is important,
- precision mechanisms, where an even and thin coating must not affect the operation of the part,
- automotive components requiring repeatability and an attractive finish,
- electrical components, where corrosion protection must not interfere with function,
- small structural parts that must be protected without geometric changes,
- applications in dry and moderately humid environments, where stable, predictable protection against corrosion matters.
How We Carry Out Electrolytic Zinc Plating at Strumet
At Strumet we treat electrolytic zinc plating as a process that must be stable and repeatable, regardless of series size or part type. We prepare each component taking into account its shape and intended use, which is why we work both on the rack line for larger components and on the barrel line intended for small parts. This allows us to match the technology exactly to the specific application. We continuously monitor the bath composition, pH, temperature and current density, because these parameters determine the coating structure and its durability. We complete everything with chromium-free passivation, so the coating retains its properties over a long period of use as well.
Electrolytic Zinc Plating in Practice - Process Control and a Stable Result
Electrolytic zinc plating is a technology that clearly shows whether the process is under control. With a well-run line the result is even, stable and predictable, and the coating simply does its job in the everyday operation of the component. At Strumet we focus precisely on making sure every part leaves the process in exactly the condition it should.
Thanks to consistent parameter control and a calm running of the process, the coating retains its properties even after a longer period of use. Components move on without surprises, and zinc plating stops being a subject for analyses and rework.





