
Steel is one of the pillars of modern construction and industry - but only when it is properly protected against corrosion. Without this, metal in contact with moisture, salts, or aggressive gases loses its mechanical properties faster than designs and maintenance schedules assume. The chosen corrosion protection technology therefore determines not only the durability of the structure but also the safety of users and the total life-cycle cost of the investment.
Galvanizing is today the most widely used method of protecting steel - cheaper than epoxy coating or stainless steel, and far more effective than painting alone. This term, however, covers several very different technologies that differ in coating thickness, method of application, range of uses, and price.
Why Does the Choice of the Right Corrosion Protection Method Matter So Much?
Corrosion is responsible for losses worth billions in industry worldwide - it destroys bridges, production halls, tanks, pipes, and load-bearing structures. In Poland, according to industry estimates, the costs of corrosion degradation consume several percent of GDP annually. For engineers and investment managers, this means one thing: choosing the right method of protecting steel surfaces should be a strategic decision.
One of the most effective and most commonly used protection methods is galvanizing of steel, that is, a technology based on applying a layer of zinc to the surface of an element. Zinc plays a dual role: it forms a physical barrier separating the metal from the aggressive environment and acts as a sacrificial anode, electrochemically protecting the substrate even where the coating is damaged. For this protection to be effective and economically justified, however, it is crucial to match the right technology to the specific service conditions.
The Most Popular Types of Galvanizing - an Overview of the Technologies
There are several basic types of zinc coating: hot-dip galvanizing, electroplating, thermal spraying, and sherardizing. Each of these methods has its strengths - what decides is the operating parameters: temperature, humidity, the presence of chemical substances, and the required service life.
Zinc Electroplating (Electrolytic Galvanizing)
In the electroplating process, electrolytic zinc is applied using an electric current in an electrolytic bath. This method makes it possible to obtain coatings 3-25 μm thick, characterized by very good uniformity and an attractive appearance. It works excellently for small parts such as connectors, bolts, screws, and electrical components exposed in environments of low to moderate corrosivity (categories C1-C2 according to ISO 9223).

Thermal Spray Galvanizing (Metallizing)
Metallizing involves spraying molten zinc, or zinc in the form of wire, onto a previously prepared, blast-cleaned surface. The coating thickness can reach 100-200 μm, which makes this method particularly valuable for on-site renovation of large structures (bridges, tanks, masts), where transporting the element to a galvanizing plant is impossible or uneconomical. Adhesion to the substrate is very good thanks to the mechanical anchoring of the zinc in the rough surface.
Sherardizing (Powder Galvanizing)
In the powder method (sherardizing), steel elements are placed together with zinc powder in a rotating drum and subjected to a temperature of about 320-500°C. The resulting diffusion zinc-iron coating has a hardness and abrasion resistance higher than with other methods; however, it is also a comparatively more expensive solution. It is used mainly to protect fasteners, nails, chains, and small parts with complex geometry.
Hot-Dip Galvanizing (Immersion)
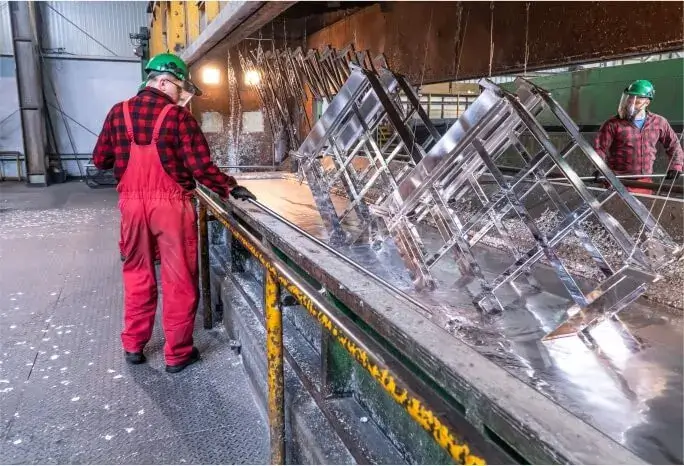
This is the dominant technology in industrial corrosion protection. The steel element is immersed in a bath of molten zinc at a temperature of about 450°C. A multilayer zinc-iron coating (eta, zeta, delta, and gamma phases) is then formed, with a thickness depending on the chemical composition of the steel and the immersion time - from 50 to 100 μm, or even thicker for reactive steels. The method is governed by PN-EN ISO 1461 - the Polish standard implemented on the basis of the European standard, which precisely defines minimum coating thicknesses, appearance requirements, test methods, and acceptance conditions.
Hot-Dip Galvanizing vs. Electroplating - Which Method to Choose?
The answer to the question of hot-dip galvanizing vs. electroplating - specifically, which of these solutions will be recommended in a given case - depends on several factors.
Zinc electroplating prevails when the priorities are:
- a small part in terms of size,
- dimensional precision (a thinner coating does not disturb tolerances),
- aesthetics,
- lower unit cost for large production runs.
In terms of coating thickness and durability, hot-dip galvanizing has no equal in environmental conditions of category C3 and higher (urban environments with moderate pollution, industrial, coastal). A hot-dip coating at a thickness of 85 μm can provide protection for 50 years or more without maintenance - confirmed not only by manufacturers but also by scientific research.
FAQ - Most Common Questions About Types of Galvanizing
Which method gives better results in terms of resistance: hot-dip galvanizing or electroplating?
Hot-dip galvanizing gives a coating several times thicker than electroplating, which translates directly into a much longer service life in harsh conditions. A hot-dip coating also has a metallurgical bond with the substrate - it is part of the steel's structure rather than merely applied to its surface. This makes it more resistant to mechanical damage, and in the case of scratches the zinc still electrochemically protects the exposed iron. The electroplating method, on the other hand, is more precise and economical for small parts exposed to mild conditions.
Is so-called cold galvanizing a full-value alternative to the zinc bath?
Cold galvanizing is the colloquial name for applying zinc-rich coatings by brush, roller, or aerosol, without heating the element or using a bath. The zinc content in such preparations is typically 85-96% in the dry coating. This method has its uses - it works excellently for repairing damaged hot-dip coatings or as a temporary solution in the field where full galvanizing is not possible. However, it should not be treated as a full replacement for the zinc bath. The absence of metallurgical diffusion, the uneven thickness of manual application, and poorer adhesion properties mean that the durability of the coating is clearly lower, especially in corrosivity categories C3-C5.
For which industries will specific types of zinc coating be the most suitable?
- Building and infrastructure construction - hot-dip galvanizing as the standard, often required by construction projects.
- Power generation and the mining industry - hot-dip, owing to corrosivity categories C4-C5.
- Automotive and household appliances - electroplating or sherardizing, owing to dimensional precision and aesthetics.
- Agriculture and water and wastewater management - hot-dip galvanizing providing many years of maintenance-free durability.
How long does a coating applied by the hot-dip method last?
The service life of a hot-dip coating depends primarily on the coating thickness and the corrosivity category of the environment. According to the ISO 9223 standard and industry data, in a C2 environment (rural, low humidity) a coating 85 μm thick can protect for over 70 years, in C3 (urban, moderate pollution) - 30-50 years, in C4 (industrial, coastal) - 15-25 years, and in C5 (very aggressive) - 7-15 years. Such estimates assume no mechanical damage and proper surface preparation before galvanizing, in accordance with the requirements of PN-EN ISO 1461.
If you are looking for a proven partner for galvanizing orders - regardless of batch size and component dimensions - Strumet offers comprehensive service. Many years of experience serving the construction, power, and industrial sectors allows us to match the technology precisely to the requirements of each project.





