Hot-dip galvanizing is one of the most effective methods of protecting steel against corrosion. With proper preparation, the zinc coating can protect a structure for 30, or even 100 years without any maintenance. The problem is that many defects that come to light only at the galvanizing plant originate much earlier – at the design stage or in the welding shop. We have collected 5 mistakes that most often complicate the galvanizing process and reduce the durability of the coating.
1. Choosing the right steel grade – the foundation of durable hot-dip galvanizing
The chemical composition of steel directly affects how the reaction with liquid zinc proceeds. The content of silicon (Si) and phosphorus (P) is particularly important. Hot-dip galvanizing gives the best results for steel with a silicon content below 0.03% or in the range of 0.15–0.25% (the so-called Sandelin effect is responsible for this). Steels with an Si content in the range of 0.03–0.14% may react excessively: the coating becomes too thick, brittle and grayish instead of shiny. A similar effect is caused by an elevated phosphorus content.
The mistake is that designers select steel solely on the basis of strength parameters, ignoring its reactivity in the zinc bath. The solution is to verify the material certificates before ordering galvanizing and – if possible – to choose steel described as "suitable for hot-dip galvanizing".
2. Process holes – a guarantee of safety and coating quality
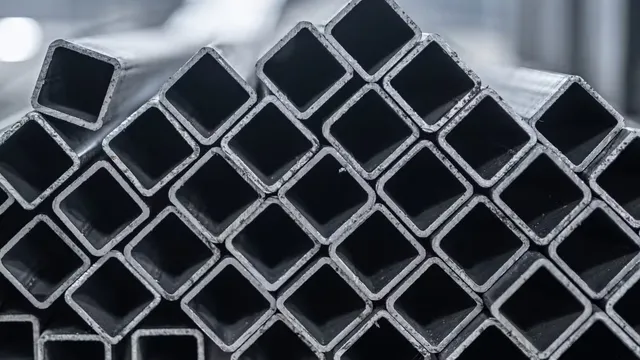
This is technically the most serious mistake, and it can have serious safety consequences. Closed profiles (tubes, boxes, enclosures) without venting and drainage, immersed in liquid zinc at approx. 450°C, may burst violently as a result of the expansion of trapped air or liquid vapors. The lack of proper drainage also has an adverse effect on quality, because zinc accumulates inside the profiles and forms thickened areas, "icicles" and places with non-uniform coating thickness.
Correctly designed holes should be located at the lowest and highest point of each closed cross-section, so that there is no need to rotate the element during the process. The minimum hole size depends on the dimensions of the profile – the detailed guidelines in force at Strumet's hot-dip galvanizing plant are presented in the table below:
| Internal dimensions of the closed profile (mm), smaller than: | Minimum hole diameter (mm) at opposite ends of the profile and their number: | ||||
| Round | Square | Rectangular | 1 hole | 2 holes | 3 holes |
| 15 | 15 | 20 × 10 | 8 | – | – |
| 20 | 20 | 30 × 15 | 10 | – | – |
| 30 | 30 | 40 × 20 | 12 | 10 | – |
| 60 | 60 | 80 × 40 | 20 | 12 | 10 |
| 80 | 80 | 80 × 60 | 20 | 18 | 12 |
| 100 | 100 | 120 × 80 | 25 | 20 | 12 |
| 120 | 120 | 160 × 80 | 30 | 25 | 16 |
| 160 | 160 | 200 × 120 | 40 | 25 | 16 |
| 200 | 200 | 260 × 140 | 50 | 30 | 16 |
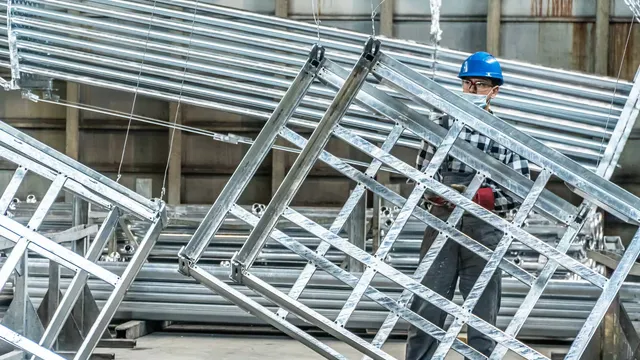
Our galvanizing plant has a bath measuring 10.2 × 1.4 × 2.7 m, which allows large and complex structures to be galvanized – but that is exactly why designing their drainage requires particular care.
3. Hot-dip vs electrolytic galvanizing – why do they require a different approach?
The difference between hot-dip galvanizing and zinc electroplating is not only the coating thickness (50–100 μm vs. 3–25 μm), but above all the different requirements for part geometry. In hot-dip galvanizing, elements are immersed in a bath of liquid zinc, so gaps and lap joints become a trap for the acids used in the pickling process. If sheets were overlapped without continuous welding, or without maintaining a gap of at least 2.5 mm with an intermittent weld, the acid is trapped between the sheets. After galvanizing, it is gradually washed out, causing under-coating corrosion and characteristic rusty "leaks".
As the Polish Galvanizers Association points out, the rule is simple: either a continuous, sealed weld, or an intermittent one with an appropriate clearance maintained. Never an overlap with no welding at all.
4. Welds and joints – how to weld so that the zinc coating does not rust at contact points?
A zinc coating is only as good as the substrate it sits on. Welding slag, spatter, unground pores and an excessively rough weld face prevent zinc from being applied evenly. In these places the layer is thinner, non-uniform or does not adhere at all – which means an entry point for corrosion.
According to industry guidelines (described, among others, by Engineer's Guide), welds intended for hot-dip galvanizing should be made using a semi-automatic gas-shielded method. Welding with coated electrodes carries a risk of poor coating quality, because the welding flux coating must absolutely be removed before galvanizing – and in practice this can be difficult with complex structures. The edges of elements should be chamfered or rounded: a sharp edge causes zinc to run off and not reach the required protective thickness.
The technological process of hot-dip galvanizing at Strumet includes inspection of the substrate before immersion, nevertheless responsibility for the quality of welds always lies with the manufacturer of the structure.
5. The duplex system, or how to prepare the surface for painting galvanized steel
If the customer plans additional painting after galvanizing (the so-called duplex system), they must know that fresh hot-dip galvanized steel is a difficult substrate for paints. The smooth, passive surface of zinc oxide bonds poorly with paint coatings – especially alkyd and epoxy ones. The solution is to carry out light abrasive sweeping (sweep blasting) or to use a primer designed specifically for zinc.
A properly selected paint for galvanized steel, applied in a duplex system, not only makes it possible to obtain any color from the RAL palette but – thanks to the synergy effect of both coatings – significantly extends the time to first maintenance compared with zinc alone or paint alone. It is estimated that the durability of a duplex system is 1.5 to 2.5 times longer than the sum of the durability of each layer separately.
FAQ – the most common questions about preparing steel for galvanizing
Does a zinc coating rust after several years of use?
The zinc coating itself does not rust – zinc is a metal that corrodes much more slowly than steel and forms stable carbonate compounds (patina) on its surface, which further slow the degradation process. If traces of rust appear on a galvanized structure, it is most often in places of mechanical damage, on sharp edges, at defective welds or – as described above – as a result of under-coating corrosion caused by design errors.
What types of zinc coating are there and which to choose for large structures?
The basic types of zinc coating are hot-dip (immersion) galvanizing and zinc electroplating (electrolytic). For large steel structures exposed to harsh weather conditions, we strongly recommend hot-dip galvanizing – it gives a coating several times thicker and more durable.
Is the galvanizing process at Strumet safe for the environment?
Yes. The Strumet hot-dip galvanizing plant operates a zero-wastewater system. The chemical baths used in the process are held in an internal closed loop – no liquid process waste is discharged into the environment.
How quickly can Strumet galvanize my order?
The lead time depends on the size and complexity of the order, e.g., for a load weight of up to 3 t, completion is possible within 10 hours. It is best to contact our sales department directly about this.
If you have doubts about the preparation of your structure, do not wait until the problem comes to light at the galvanizing plant. Contact us already at the design stage – we will help you avoid costly rework and ensure a coating that will protect your steel for decades.